Quick Answer
A Linija za ekstrudiranje cevi iz PE-ja is an industrial production system that is used to manufacture polyethylene pipes and tubes continuously and with a controlled diameter, wall thickness, length, and surface quality. According to ISO 4427, polyethylene piping systems are widely used for water supply and related applications. Meanwhile, industry extrusion systems extend PE pipe production to include gas distribution, irrigation, drainage, industrial fluid handling, marine pipelines, and protective or insulated piping. The extrusion process generally involves feeding, melting and plasticising the material, forming it in a die, sizing it, cooling it, hauling it, cutting or winding it, and carrying out online quality control.
In practical manufacturing, the value of a PE pipe tube extrusion line lies not only in its ability to produce plastic tubes, but also in its capacity to convert PE resin into continuously dimensioned pipes designed for specific applications and performance requirements. Depending on factors such as the resin grade, pipe diameter, wall thickness, pressure class, production speed, and end use, the line can be configured to produce small-diameter flexible tubing, standard HDPE water pipes, gas pipes, irrigation pipes, large-diameter infrastructure pipes, or specialised PE protective pipes.
What Is a PE Pipe Tube Extrusion Line?
A PE pipe tube extrusion line is a continuous manufacturing system designed to transform polyethylene resin into finished pipes or tubes. Unlike batch moulding processes, extrusion produces a continuous hollow profile by melting polymer pellets, forcing the molten material through an annular die, shaping the hot tube with calibration and cooling equipment, and then pulling the stabilised pipe through downstream machinery.
The term ‘PE pipe tube extrusion line‘ covers a broad range of equipment because polyethylene products are manufactured in many different diameters and configurations. Small-diameter PE tubing can be wound directly into coils, whereas large-diameter HDPE pipes are usually produced as straight lengths and require multiple haul-off tracks, large vacuum tanks, heavy-duty cutting equipment and automated stacking. Therefore, the equipment configuration needs to be matched to the intended pipe specification rather than being selected only according to the polymer name.
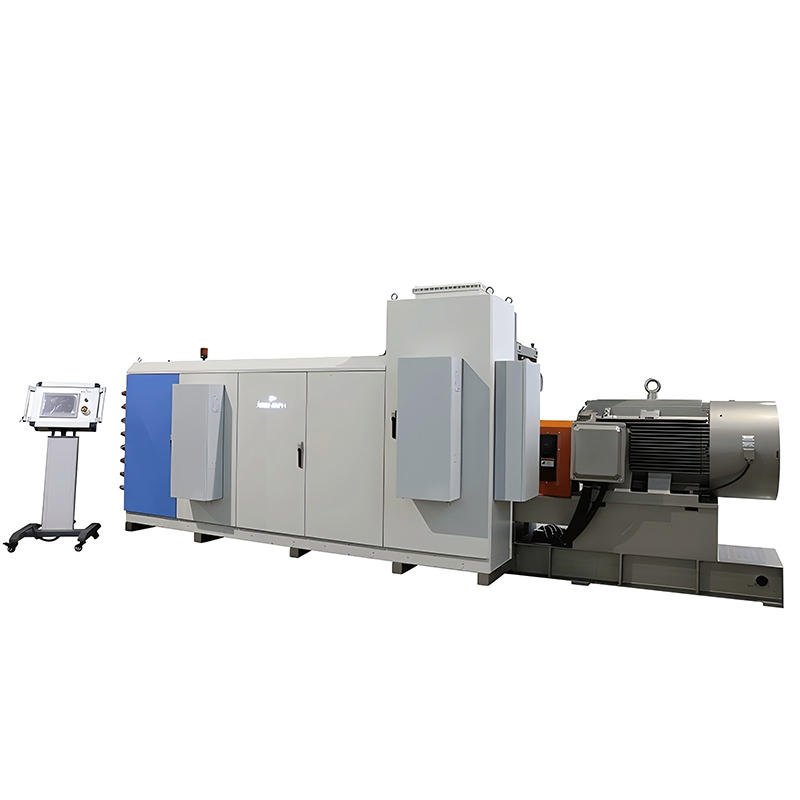
A typical production system contains a material feeding unit, a hopper or a gravimetric dosing system, a single-screw extruder, an extrusion die, a vacuum calibration tank, a cooling section, a haul-off unit, a cutter or a winder, and pipe handling equipment. Modern systems may also incorporate laser diameter measurement, online wall thickness monitoring, meter weight control, automatic marking, and centralised PLC/HMI control. These components work together as a single process chain because dimensional accuracy depends on synchronising melt output, die pressure, cooling, traction speed and downstream handling.
What Materials Can a PE Pipe Extrusion Line Process?
Polyethylene is not a single material grade. The manufacture of PE pipes can involve high-density polyethylene (HDPE), medium-density polyethylene (MDPE) and other polyethylene formulations, which are selected according to factors such as pressure requirements, flexibility, environmental conditions, chemical exposure, temperature and the relevant pipe standard. HDPE is particularly important in infrastructure because it combines high strength with flexibility, corrosion resistance, and good fusion characteristics.
The resin grade directly affects the design and operating conditions of the extrusion line. For example, a material intended for a large-diameter pressure pipe may require a different screw configuration, output capacity, cooling strategy, and haul-off arrangement than a small-diameter irrigation tube. Material preparation is equally important, as consistent feeding and a stable melt temperature help to prevent dimensional fluctuations, surface defects, and variations in wall thickness.
Some modern pipelines can also be configured for multilayer production. Additional extruders can be integrated to manufacture two- or three-layer PE pipes, enabling different material formulations or functional layers to be incorporated into the same pipe structure. This flexibility is useful when manufacturers need to combine performance, colour identification, recycled material content, and application-specific surface characteristics in one product.
How Does a PE Pipe Tube Extrusion Line Work?
The manufacturing process begins with the PE resin being fed into the extruder. Inside the barrel, the polymer is transported forward by rotating screw flights while heat and mechanical shear progressively melt and homogenise the material. The screw and barrel system must be designed so that it delivers a stable melt with consistent temperature and pressure, because fluctuations at this stage can eventually result in variations in wall thickness, surface defects, or unstable pipe dimensions.
The homogeneous polymer melt then enters the die head, where it is distributed around a central mandrel to create a continuous tubular profile. The material is still hot and relatively soft at this point, so controlled sizing and cooling are required for it to retain the final dimensions. The pipe therefore passes through a calibration system involving vacuum sizing to achieve the desired pipe geometry, followed by water cooling to remove heat and stabilise the polymer.
Once the pipe has reached sufficient dimensional stability, a haul-off unit pulls it continuously through the line. The relationship between extrusion output and haul-off speed is critical: if the line pulls too quickly relative to the rate at which the material is output, the walls of the pipe may become too thin; if the traction is too slow, the pipe may become oversized or excessively thick. Modern extrusion systems therefore increasingly use synchronised control to maintain stable production conditions. Jwell’s PE and HDPE pipe systems, for instance, incorporate extrusion, vacuum sizing, cooling, a servo-driven haul-off unit, a cutting unit and centralised control, with the option of adding online measurement systems for production monitoring.
What Are the Main Applications of PE Pipe?
The largest application areas for polyethylene (PE) pipes include water supply, gas distribution, irrigation, drainage, industrial fluid transportation, mining, marine infrastructure, and protective piping. PE is widely used in these areas thanks to its corrosion resistance, flexibility, relatively low weight, and the fact that pipes can be joined through heat fusion techniques in suitable applications.
In water infrastructure, PE pipes can transport potable water and other water supplies when the material, pipe construction, and certification meet the applicable requirements. Appropriately specified polyethylene pipe is widely used for gas distribution because PE does not corrode in the same way as conventional metallic pipe, and it can accommodate ground movement more readily than rigid materials in many installation conditions.
Agricultural irrigation is another major market for smaller PE pipes and tubes. These products can be manufactured in continuous lengths and wound into coils, which simplifies transportation and field installation. Depending on the design, PE extrusion lines can also produce pipes for drainage, agricultural water delivery, cable protection, and other low- to medium-pressure applications.
Large-diameter PE extrusion expands the range of applications into municipal infrastructure, industrial water systems, dredging and marine pipelines. Therefore, equipment manufacturers offer substantially different line architectures for small tubes and large pipes. Published Jwell equipment information, for example, includes large-diameter HDPE systems covering pipe ranges extending into the metre scale. This demonstrates how extrusion line configuration changes substantially as diameter and throughput increase.
PE Pipe Applications and Corresponding Production Requirements
The relationship between application and machine configuration is important for anyone purchasing a PE pipe extrusion line. A manufacturer should not specify the line only from a desired output number because pipe diameter, wall thickness, resin grade, pressure class, cooling requirements, and product handling can all influence the equipment configuration.
| PE Pipe Application | Typical Product Characteristics | Important Extrusion-Line Requirements |
| Water supply | Pressure-rated PE pipe, multiple diameters | Stable melt output, precise sizing, controlled cooling |
| Gas distribution | Pressure-rated PE pipe with controlled dimensions | Consistent wall thickness, reliable process control, marking |
| Agricultural irrigation | Small or medium diameter pipe/tube, often coiled | High-speed extrusion, efficient cooling, winder capability |
| Drainage | Solid-wall or specialized drainage pipe | Appropriate die and sizing system, dimensional stability |
| Industrial fluid transport | Application-specific diameter and pressure class | Material compatibility, robust extrusion and cooling |
| Marine pipelines | Large-diameter HDPE pipe | High extrusion capacity, heavy-duty haul-off and handling |
| Cable or pipe protection | Tubes and protective conduits | Surface quality, dimensional control, flexible production |
| Pre-insulated piping | HDPE outer protective jacket | Accurate diameter, roundness, and stable surface quality |
| Mining applications | Heavy-duty PE pipe | High throughput, thick-wall capability, reliable cooling |
| Multilayer pipe | Two- or three-layer construction | Multiple extruders and synchronized layer distribution |
The table illustrates why “PE pipe extrusion machine” and “PE pipe production line” are not necessarily interchangeable specifications. A small-diameter irrigation tube and a 1,000 mm infrastructure pipe may both be PE products, but their extrusion capacity, die dimensions, cooling system, haul-off configuration, and handling requirements are fundamentally different.
What Equipment Does a PE Pipe Tube Extrusion Line Include?
Although the extruder is the core of the system, it is just one component of a complete production line. A modern line can be better understood as a coordinated manufacturing system, where the quality of the final pipe is affected by every downstream unit.
The first stage is material handling. Resin is delivered to the extruder by automatic feeders or vacuum conveying systems, while gravimetric dosing improves control of material throughput and formulation. The extruder then melts, mixes, and conveys the polymer; barrel temperature zones and screw geometry control the processing conditions in this stage.
The die head determines the distribution of the molten polymer into the tubular shape. After leaving the die, calibration and cooling equipment control the external dimensions and roundness. Vacuum calibration is particularly important for maintaining stable geometry, while multi-stage water cooling enables heat to be removed gradually rather than suddenly.
The haul-off provides controlled traction. For large-diameter pipes, several crawler tracks may be required to distribute the pulling force evenly and prevent damage to the pipe surface. Depending on the product, the line may use a chipless or saw cutter, an automatic stacker or a winder. Optional additional equipment can include laser marking systems, laser diameter measurement systems, gravimetric control systems, wall-thickness monitoring systems, belling machines and mixers.
What Determines PE Pipe Extrusion Line Output?
The output of an extruder is determined by much more than just the power of its motor. The effective production rate depends on the following factors: screw diameter and design; screw speed; polymer grade; melt temperature; die design; pipe diameter; wall thickness; cooling capacity; haul-off speed; and the stability of the entire process.
For small-diameter products, a dual-strand configuration can increase productivity by producing two pipes simultaneously, rather than doubling the number of production lines. Jwell’s small-diameter PE/PPR/PE-RT/PA line, for instance, features dual-pipe configurations for products measuring 16–75 mm and includes servo-controlled haul-off and optional winding or cutting equipment.
At the other end of the scale, large-diameter HDPE pipe requires much higher material throughput and more substantial downstream equipment. Published specifications for one Jwell HDPE pipe system show models ranging from 400–800 mm to 2,000–3,000 mm, with increasing listed outputs as the line configuration becomes larger and more powerful. However, these figures are supplier-specific reference values rather than universal industry standards, so production capacity should always be confirmed through a material trial using the buyer’s actual resin and pipe specification.
What Quality Factors Should Manufacturers Control?
The most important quality variables in PE pipe extrusion are outside diameter, wall thickness, roundness, weight per metre, surface condition, material uniformity, and dimensional stability. As these parameters are interconnected, correcting one process variable without understanding the effect on the rest of the line can create another problem.
Melt temperature and pressure must be kept stable to prevent inconsistent polymer flow, which can result in uneven wall thickness or surface fluctuations. The pipe must then be cooled uniformly by the calibration and cooling processes so that it retains its required dimensions after leaving the sizing section. Haul-off speed must be synchronised with extrusion output, as even a stable die cannot compensate indefinitely for an unstable traction ratio.
Online monitoring can significantly reduce the time between a process deviation being detected and corrective action being taken. Laser diameter measurement can continuously monitor the external diameter, while meter-weight control can help identify changes in material output. For high-value or pressure-rated pipes, manufacturers should also maintain documented laboratory testing procedures that cover the relevant mechanical and hydrostatic performance requirements of the applicable standard.
For buyers, this means that evaluation of the production line should focus on process stability rather than maximum theoretical output. A machine capable of producing 1,000 kg/h would not necessarily be more useful than a lower-output system if the application required tight dimensional tolerances and consistent production over long operating periods.
How to Choose the Right PE Pipe Tube Extrusion Line?
Rather than starting with the machine, the first step is to define the finished pipe. The buyer should specify the material grade, pipe diameter range, wall thickness or SDR requirements, applicable pressure class, required output, production length, coiling or cutting method, colour, multilayer requirements, target market and standard.
The second step is to determine the production range. A line optimised for pipes with a diameter of 20–110 mm is fundamentally different from one intended for pipes with a diameter of 630–1,600 mm. Small-diameter lines can prioritise high line speed, compact cooling systems and winding, whereas large-diameter lines require high melt throughput, powerful haul-off systems, extended cooling capacity and heavy-duty handling equipment.
The third step is to evaluate automation and quality control. PLC/HMI systems, automatic temperature control, servo haul-off, online diameter measurement, and meter-weight control can reduce manual intervention and improve repeatability. However, automation should be selected according to actual production requirements rather than being treated as a collection of marketing features.
When evaluating a PE pipeline from a supplier such as our Jwell, it is important to look beyond the headline output and examine the complete process configuration, including the extruder design, die structure, vacuum sizing, cooling capacity, haul-off arrangement, cutting or winding system, control architecture, and optional online inspection. Jwell’s published PE/HDPE systems illustrate configurations ranging from small-diameter, single- or dual-pipe production to large-diameter HDPE lines. Therefore, the exact model and technical configuration should be matched to the intended product, rather than being selected from a generic capacity table.
FAQ About PE Pipe Tube Extrusion Lines
- Za kaj se uporablja linija za ekstrudiranje cevi iz PE-ja?
A PE pipe tube extrusion line is used to continuously manufacture polyethylene pipes and tubes with controlled dimensions and wall thickness. Common applications include water supply, gas distribution, irrigation, drainage, industrial fluid transport, and protective piping.
- What materials can a PE pipe extrusion line process?
PE extrusion lines can be configured for polyethylene materials such as HDPE and MDPE, depending on the product specification and machine design. Some systems can also be adapted for related polyolefin materials or multilayer structures.
- How does a PE pipe extrusion line work?
The line melts PE resin in an extruder and pushes the homogeneous melt through an annular die to form a tube. Vacuum sizing, cooling, haul-off, and cutting or winding then stabilize and finish the pipe.
- What pipes can be produced by a PE extrusion machine?
A suitable PE extrusion machine can produce small-diameter tubes, irrigation pipes, water pipes, gas pipes, industrial pipes, and large-diameter HDPE pipelines. The actual diameter and wall-thickness range depend on the extruder, die, calibration system, and downstream equipment.
- What determines the output of a PE pipe extrusion line?
Output depends on screw design, extruder size, polymer grade, pipe diameter, wall thickness, screw speed, die design, and cooling capacity. A stable production rate should be confirmed through testing with the actual PE resin and finished-pipe specification.
- How do I choose a PE pipe tube extrusion line?
Start with the finished pipe specification, including material, diameter, wall thickness, application, output, and applicable standard. Then select the extruder, die, sizing, cooling, haul-off, cutting or winding, and automation systems that can reliably meet those requirements.
Zaključek
A PE pipe tube extrusion line is essentially a continuous polymer processing system designed to turn polyethylene resin into dimensional pipes for use in infrastructure, utilities, agriculture, industry, and specialised applications. The extruder establishes melt quality, the die creates the tubular geometry, and the haul-off controls production speed. Calibration and cooling then establish dimensions, and cutting, winding, and inspection equipment convert the stabilised pipe into a usable commercial product.
Therefore, the most important consideration when selecting such a line is not simply maximum output. The right system must match the PE material grade, pipe diameter, wall thickness, application, production capacity, quality standard, and downstream handling method, while providing sufficient process control to ensure consistent dimensions during continuous production. When comparing extrusion equipment, manufacturers should evaluate the entire process chain and validate the line using the actual resin and pipe specifications, rather than comparing extruder power or advertised capacity alone.
 English
 Russian
 Spanish
 Arabic
 German
 French
 Persian
 Turkish
 Bulgarian
 Czech
 Dutch
 Greek
 Indonesian
 Japanese
 Korean
 Polish
 Portuguese
 Romanian
 Slovenian
 Ukrainian